 RCM Auto
Explore our integrated portfolio of OEM auto accessories, EV systems, and structural vehicle components manufactured under rigorous ISO/IATF quality controls.




Delivering uncompromised structural integrity, metallurgical excellence, and high-throughput production capacities for global automotive supply chains.
Founded in 2003, Ningbo RCM Auto Accessories Co., Ltd. has established itself as an authoritative leader in auto equipment, automotive lighting, and structural components across China. Situated in Ningbo—a world-renowned hub for advanced automotive lighting and metallurgical engineering—our facility covers over 33,000 square meters housing 20 highly automated production lines.
With an annual sales volume exceeding $25 million and a 35% year-over-year export performance increase, our facility empowers tier-1 original equipment manufacturers (OEMs) and major international buyers including HELLA, Ruralking, Z-Flash, and Sinotruk.
Our operational ethos centers around one core mission: Make Vehicle Operation Safer! Supporting this commitment is a dedicated 15-person Quality Control team executing a rigorous four-stage quality assurance protocol spanning raw aluminum block verification, dynamic flow-forming inspection, spectral metallurgical scanning, and packaged goods stress testing.
Proven Reliability Benchmark: Maintained a continuous 7-year track record of 0% repair rate, 0% return rate, and zero customer complaints across global commercial exports.
Analyzing structural dynamics, aluminum alloy metallurgy, and manufacturing processes required for modern passenger, EV, and commercial vehicle architectures.
Modern car rims demand an optimized balance of tensile strength and weight reduction. Our manufacturing setup utilizes 6061-T6 aerospace-grade forged aluminum and flow-forming rim processing. Flow-forming technology applies intense hydraulic pressure to the rim barrel while spinning, re-aligning the aluminum grain structure to achieve cast-iron toughness with a 22% weight reduction compared to conventional gravity casting.
Electric vehicle (EV) adoption requires specialized wheel designs. Our EV-specific alloy rims integrate closed-surface aero-blades that cut drag coefficients by up to 8.5%. Reducing rotational inertia directly expands EV battery range while maintaining heat dissipation channels for high-torque regenerative braking systems.
Every wheel rim profile undergoes intensive FEA digital simulation prior to tooling. We analyze cornering fatigue, radial load tolerance, and sudden curb impacts. This ensures maximum load capacity ratios (exceeding 950 kg rating per wheel for heavy commercial SUVs and light trucks) while optimizing unsprung weight for enhanced vehicle handling.
| Manufacturing Technology | Material Composition | Tensile Strength (MPa) | Weight Savings vs Cast | Target Automotive Class |
|---|---|---|---|---|
| 1-Piece Monoblock Forged | Aluminum 6061-T6 | ≥ 310 MPa | 30% to 35% Weight Reduction | Hypercars, Motorsports, Premium EVs |
| Flow-Formed (Hybrid Forged) | A356.2 Aluminum Alloy | ≥ 260 MPa | 18% to 25% Weight Reduction | OEM Mid-to-Luxury Passenger Vehicles |
| Low-Pressure Precision Cast | A356 Silicon-Aluminum | ≥ 220 MPa | Baseline Reference | Mass Market Passenger & Commercial Fleet |
| Heavy Duty Forged Truck Rims | High-Density Alloy 6061 | ≥ 340 MPa | 20% Weight Reduction (vs Steel) | Heavy Duty Trucks, Buses, Commercial Trailers |
Navigating global supply chain dynamics, regional regulatory requirements, and raw material sourcing strategy.
China accounts for over 45% of the world's automotive wheel rim manufacturing output. The combination of localized aluminum smelting infrastructure, advanced robotic CNC machining centers, and comprehensive finishing networks gives Chinese wheel suppliers an unmatchable competitive edge in speed-to-market, cost-efficiency, and scale.
Ningbo RCM leverages these regional supply chain advantages, coupling them with western-standard engineering protocols. By maintaining an in-house rapid prototyping laboratory, custom wheel designs transition from CAD renderings to physical samples within 7 days, and full complex tooling within 20 to 25 days.
Global automotive distributors face strict regulatory compliance burdens across different continent sectors:
How Ningbo RCM maintains 0% return rates across international commercial shipments.
To guarantee rim integrity, 100% of our manufactured alloy wheel blanks pass through automated X-ray structural inspection scanners. This detects micro-air inclusions, shrink porosity, and subsurface voids that could lead to catastrophic high-speed failure.
Rims endure severe weather conditions, road salt, and brake dust oxidation. Our finishing process incorporates electro-coating pretreatment, a 3-layer liquid painted finish, and clear protective acrylic lacquers validated under a 96-hour continuous CASS salt-spray test chamber.
We provide comprehensive white-label and OEM customization. From custom offsets (ET), bolt patterns (PCD), center bore sizing, color anodization, and laser-engraved branding, our engineering unit turns bespoke buyer specifications into mass-producible components.
Engineered hardware and vehicle accessories tailored to severe industrial and fleet usage environments.
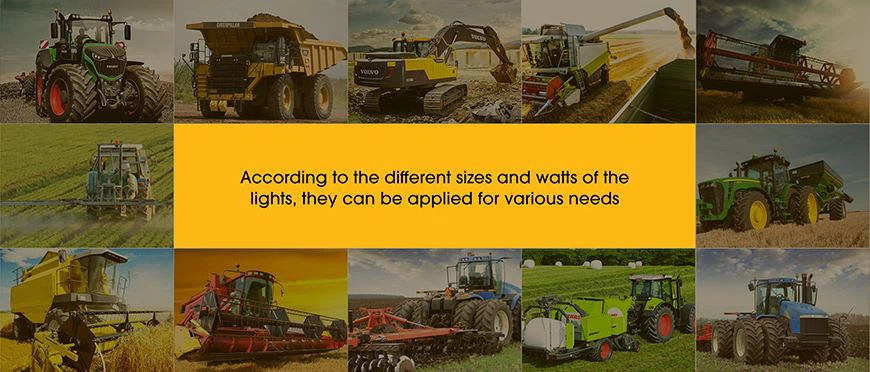
Emergency response vehicles (Police Cars, Ambulances, Fire Engines, Rescue Units) demand maximum structural integrity under sudden high-speed cornering and curb jumps. Combined with our emergency warning lighting systems, our wheel assemblies and structural hardware deliver zero-fail operational dependability for first responders.
Heavy duty earth-moving equipment (Excavators, Mining Dump Trucks, Cranes, Road Rollers) operates in high-abrasion environments. Wheel rims and chassis parts require heavy radial load capacities exceeding standard commercial thresholds, manufactured with reinforced steel and thick forged aluminum alloys.
Long-haul semi-trucks, trailers, and public transit buses benefit tremendously from forged aluminum rim upgrades. Replacing heavy steel rims cuts unsprung weight by up to 300 kg per truck-trailer combination, resulting in improved fuel economy and reduced axle wear.
High-end passenger EVs and luxury sport SUVs require specialized multi-spoke low-drag alloy wheels. Customized PCD and offset configurations accommodate oversized performance brake calipers while elevating modern aesthetic appeal.
Pioneering future-ready wheel rim design, carbon-composite integration, and AI-driven automated quality inspection.
By leveraging artificial intelligence algorithms, future rim geometries are designed organically to eliminate unnecessary material while placing structural mass strictly along stress vectors. This process reduces alloy consumption by 12% without forfeiting rigidity.
Our R&D team is advancing hybrid rim construction—coupling a lightweight forged aluminum alloy hub with a woven carbon fiber barrel. This hybrid architecture delivers a massive 40% reduction in rotational inertia, tailored for ultra-high performance EV platforms.
Integrating strain gauges and real-time thermistors directly inside the inner rim barrel. Connected via IoT modules, these smart rims provide fleet operators with continuous live data on tire pressure, structural load strain, and wheel bearing temperature anomalies.
Discover our complete range of certified brake components, security electronics, maintenance equipment, and cabin accessories.


Expert answers regarding OEM sourcing, manufacturing lead times, quality testing, and technical specifications for global car rim buyers.


